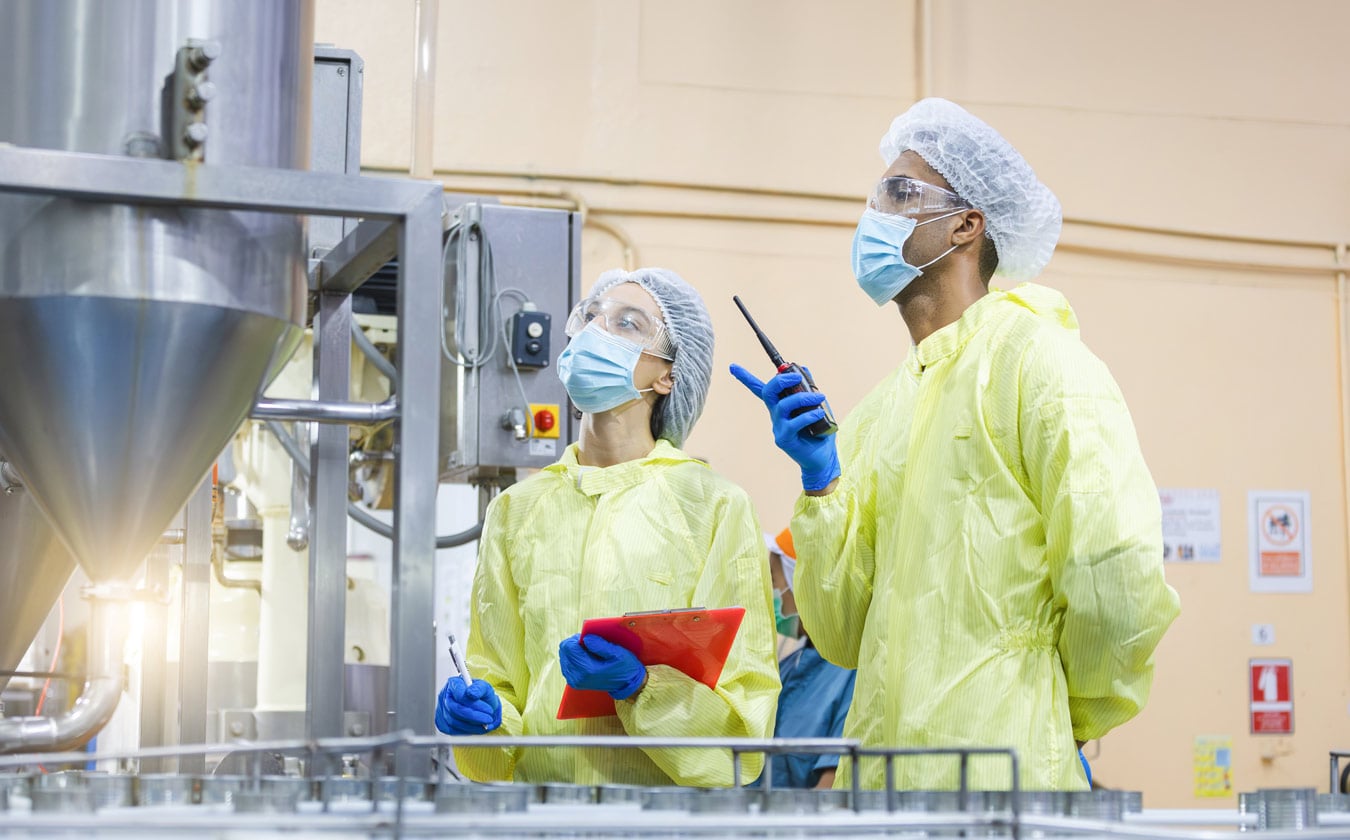
In the fast-paced world of food processing, maintaining optimal inventory levels while ensuring efficiency and compliance can be a significant challenge. At Nelson-Jameson, we understand these complexities and are dedicated to providing solutions that empower your success. In this article, we share just some of the benefits of Vendor Managed Inventory (VMI), a powerful approach that can transform your inventory management processes and contribute directly to your bottom line.
The advantages of VMI for your food manufacturing operations
Implementing a VMI system offers a multitude of advantages specifically tailored to the unique demands of food processing plants. Let's delve into some of the key benefits:
- Reduced risk of stockouts and enhanced availability: In food manufacturing, running out of essential supplies – whether it's cleaning chemicals, personal protective equipment (PPE), or testing materials – can lead to costly production delays and even impact food safety compliance. VMI helps mitigate this risk by providing real-time inventory visibility to your vendor, allowing for proactive replenishment before stock levels become critical. This ensures that the items you need are always available when needed, boosting productivity and reducing downtime.
- Optimized inventory levels and reduced costs: Traditional inventory management often involves a balancing act between overstocking (tying up valuable capital and increasing storage costs) and understocking (risking production halts). VMI leverages data-driven insights to optimize your inventory levels. By analyzing your usage patterns and sales data, we can ensure that stock is replenished only when necessary, reducing overstock, minimizing waste from expired materials, and lowering carrying costs. Many facilities see significant inventory reductions after implementing vending solutions.
- Streamlined Operations and Improved Efficiency: Managing inventory can be a time-consuming process, involving tasks like monitoring stock levels, generating purchase orders, and tracking shipments. VMI automates many of these tasks, freeing up your personnel to focus on core production activities and other value-added responsibilities. The reduction in administrative burden and the elimination of manual ordering errors contribute to significant gains in efficiency.
- Enhanced Forecasting and Planning: The continuous flow of data inherent in a VMI partnership provides both you and your vendor with a clearer picture of demand patterns and trends. This improved visibility allows for more accurate forecasting, leading to better production planning and more efficient resource allocation. Vendors can also analyze data from multiple retailers to recognize and plan for local trends.
- Increased Accountability and Reduced Loss: With VMI, the responsibility for maintaining optimal stock levels shifts to your vendor. This shared responsibility, coupled with the transparency of inventory data, can lead to increased accountability and a reduction in product loss due to spoilage, damage, or even internal misuse. Knowing who accessed what and when can foster more responsible consumption habits.
- Stronger Supplier Relationships: VMI fosters a closer, more collaborative relationship between your food processing plant and Nelson-Jameson. By working together towards shared goals, we can develop a deeper understanding of your specific needs and challenges, allowing us to provide even more tailored and effective solutions. This symbiotic relationship builds trust and strengthens long-term business prospects.
- Support for Regulatory Compliance: Compliance with stringent regulations is paramount in the food processing industry. VMI can support your compliance efforts by ensuring that critical safety equipment and testing supplies are always available and properly managed. Detailed reporting features can also provide valuable documentation for audits and inspections.
'Expert logistics to get you what you need when you need it' with Nelson-Jameson
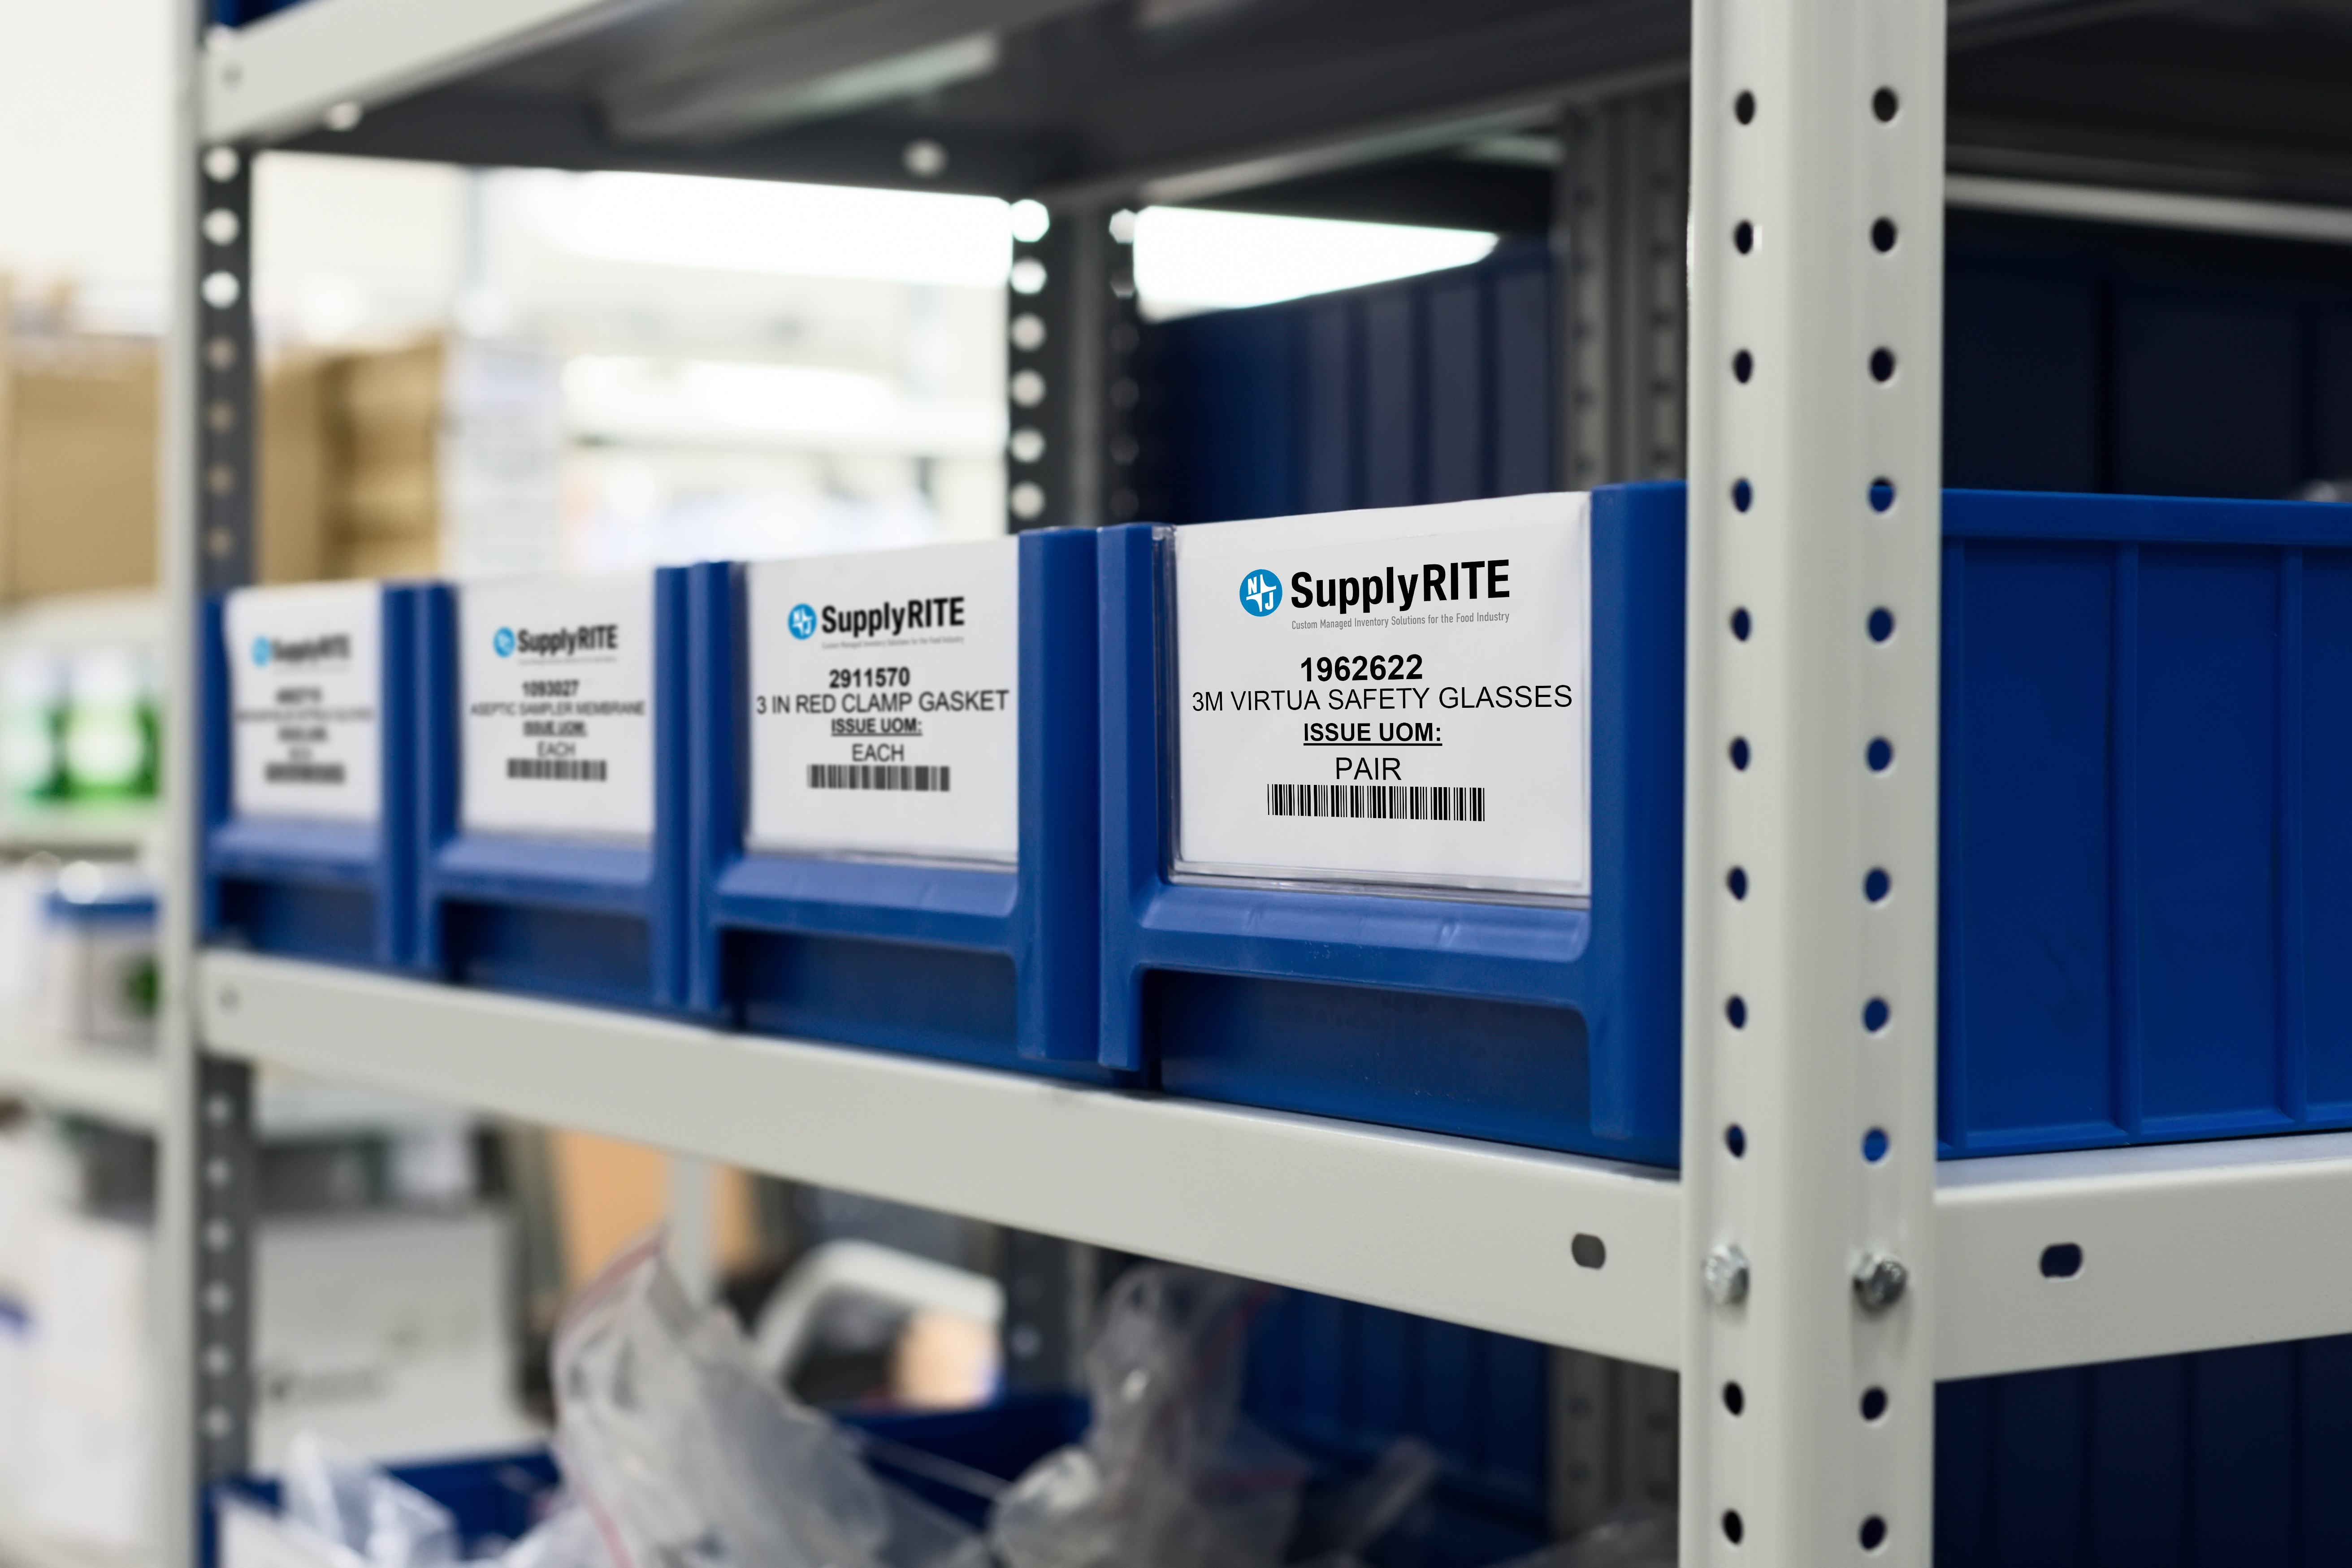
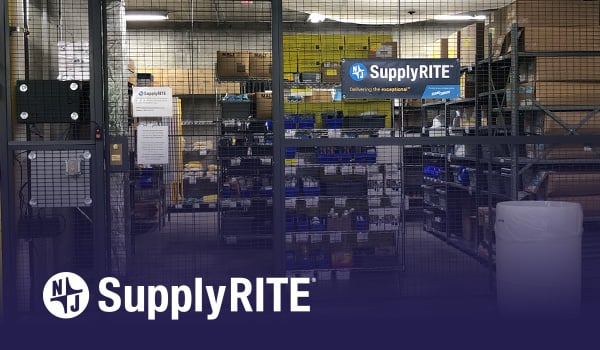
At Nelson-Jameson, we don't believe in one-size-fits-all solutions. We take a proactive and resourceful approach to understanding your unique inventory challenges and operational goals. Our SupplyRITE™ inventory management solutions, including industrial vending machines, are designed to be flexible and adaptable to your specific needs, whether you prefer a fully customer-managed or a completely Nelson-Jameson vendor-managed inventory (VMI) approach..
Contact our team today to learn more about how our SupplyRITE™ solutions and VMI programs can be tailored to meet your specific needs and contribute to your ongoing success. Let us be your trusted partner in Delivering the exceptional™ in inventory management.